If you’re in food packaging printing, you already know how tiny details make or break a run—literally. I’ve been an anilox sleeve supplier for 7 years, and one question I get every week is, “Wait, do I even need to worry about which anilox sleeve I pick for food packaging?” The short answer? Hell yeah, you do. Food packaging isn’t like printing a random poster; it’s for stuff people eat. Not only do you have to make sure the ink transfers perfectly so your chips bag looks crisp or your frozen pizza label doesn’t smudge in the freezer, but you also have to follow strict food safety rules. Let’s break down the real, on-the-ground considerations I walk every customer through, no boring textbook jargon (I save that for the data sheets). Anilox Sleeve
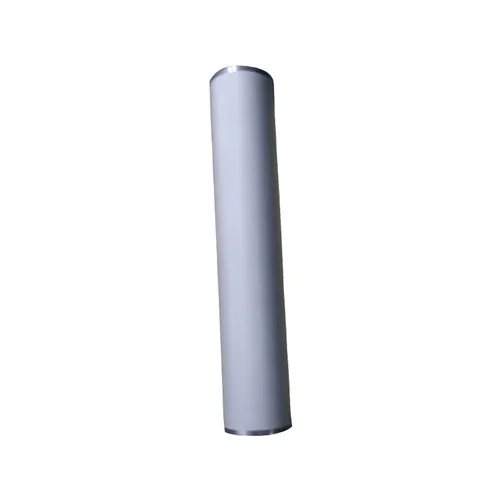
First off, food-grade compliance is non-negotiable. I can’t tell you how many times a customer has called me panicking because their old sleeves had a chemical leach that failed a third-party test. Here’s the thing: not all anilox sleeves are made the same. The old metal ones (think chrome-plated steel) are cheap, but if you’re printing food packaging, that chrome can flake over time, or the solvents in food-safe inks can eat away at the coating. Most packaging plants use flexo printing these days, right? Flexo relies on the anilox sleeve to meter ink evenly—too much ink and you get smudges, too little and your design is faded. But if the sleeve’s material isn’t food-safe, you’re not just looking at a print fail; you’re looking at a product recall, lawsuits, and a brand’s reputation that’s sunk.
When I’m advising a food client, I always push them to ask for FDA-compliant or EU 10/2011 certified sleeves. Wait, let’s be real—don’t just take the supplier’s word for it. Ask for the actual test reports. Last year, a mid-sized snack company bought some cheap sleeves from a fly-by-night supplier, printed 50,000 bags of granola, and the lab found trace amounts of heavy metals in the ink that transferred to the packaging. They had to toss every bag, lose $80k, and their production line was down for 3 days while they waited for replacement sleeves. I ended up swapping them for our food-grade ceramic sleeves (we use a baked-on ceramic coating that’s inert, no leaching) for a small upcharge, and they’ve been a customer ever since. The bottom line: skimping on compliance here isn’t just risky—it’s expensive.
Next up, the anilox cell count and volume. This is where new print guys zone out, but if you mess this up, your food packaging will look like garbage. Let’s keep it simple: the anilox sleeve has tiny cells (like microscopic wells) that hold ink. The count is how many cells are per square inch, and the volume is how much ink each cell holds. For food packaging, the inks are often water-based or have low-VOC solvents (better for food contact, less smelly, but trickier to work with). So if you pick a sleeve with too high a cell count (like 600 LPI, lines per inch), the cells are tiny, can’t hold enough low-viscosity ink, and your design will be patchy. Too low a cell count (say, 150 LPI) and you’ll overload the ink, leading to transfer issues—think ink rubbing off on people’s fingers when they open a cereal box.
Wait, let’s use a real example. A frozen food brand came to me a few months back, their labels were streaky and the black text on the microwaveable meals looked blurred. They were using a 400 LPI sleeve for all colors, but their main ink was a dark, water-based black that needed a higher volume. We swapped them to a 380 LPI (slightly lower, higher volume) sleeve for the black, and kept 450 LPI for the lighter colors. Fixed their streak issue immediately. The key here is to match cell count and volume to both the ink type and the specific substrate (what you’re printing on). Food packaging uses all sorts of substrates—polyethylene for milk jugs, paper for cereal boxes, laminated film for frozen dinners. Each one needs a different ink transfer, so the sleeve can’t be a one-size-fits-all. I always ask clients to send me their ink specs and substrate samples before I recommend anything—saves them from wasted runs.
Then there’s wear and tear, and sanitation. Food packaging lines run 12-16 hours a day, 6 days a week, and they’re super dirty. You’ve got food residue, ink buildup, maybe even occasional spills of oil or cheese stuff (yes, really). If your anilox sleeve isn’t durable, it’ll wear out fast—cells will get distorted, volume will drop, and ink transfer will get wonky. But here’s the twist: durable doesn’t mean you can skip cleaning. Ceramic sleeves are way more durable than chrome ones—they can handle 2-3 times more runs before you have to replace them—plus they’re easier to sanitize. Wait, why does sanitizing matter? Because leftover ink in the anilox cells can breed bacteria, and if you’re printing packaging for perishables (like raw meat or fresh produce), that’s a huge food safety no-no.
I tell all my food packaging clients two things here: first, invest in ceramic-coated sleeves (we use a dense, micro-crystalline ceramic that resists scratches and ink buildup). Second, don’t skip the automated cleaning cycles. A lot of guys try to cut corners and just wipe the sleeve down manually, but that leaves residual ink in the tiny cells. We also offer a one-year maintenance check for our food-grade sleeves—we come to their plant, do a scan of the cell volume, touch up any minor wear, and adjust it so they don’t have to replace the sleeve prematurely. Last year, a plant that printed organic produce bags was having issues with mold growing in their anilox cells—switched to our ceramic sleeves and started using our recommended ultrasonic cleaning method, and the mold issue was gone in 2 weeks. The sleeve lasted them 3 years instead of 18 months, so they saved money long-term.
Substrate-specific needs are another big one, and I see this all the time. Food packaging substrates aren’t just plain paper—they’re coated, uncoated, laminated, even foil-based. Let’s take flexible packaging, which is huge for snack foods. Flexible film (like the potato chip bags) is thin, stretchy, and smooth. For that, you need an anilox sleeve with a slightly textured surface so the ink adheres without beading. If you use a sleeve that’s too smooth, the ink will sit on top of the film and scratch off when the bag is filled and sealed. For rigid substrates, like cardboard for cereal boxes, you need a higher cell volume to get the ink to soak into the paper fibers evenly, so the text and images don’t look washed out.
A bakery client hit me up last month—they were printing their cookie boxes on matte cardboard, and the text was fading after a few weeks on the shelf. They’d been using a chrome sleeve that wasn’t calibrated for matte stock. We recommended a food-grade ceramic sleeve with a higher volume (12 BCM, billion cubic microns) for the solid text areas, and 20 BCM for the background graphics. Within the first production run, the text was sharp, and when they tested boxes after a month in storage, no fading. The key here is to stop treating anilox sleeves as a commodity part—they’re a critical link in how your packaging turns out, and it’s tailored to what you’re printing. I always joke with clients that if their sleeve is wrong, even the best design and most expensive ink won’t save their packaging from looking cheap.
Oh, and let’s talk about solvent compatibility, because this is tied to food safety and print quality. Food packaging inks are mostly water-based now, for environmental reasons, but some specialty packaging uses alcohol-based solvents. Both are safer than old petroleum-based inks, but they can react with the sleeve’s coating. If you use a sleeve made for petroleum inks with water-based ink, the ceramic coating can break down over time, leading to leaching or cell damage. Last year, a client who printed soy sauce bottles used a petroleum-based ink sleeve with a water-based ink and started noticing pinholes in the packaging (tiny holes where the ink didn’t transfer) after 10,000 runs. We switched them to a sleeve formulated for water-based food inks, and the pinhole issue vanished. The sleeve’s coating is engineered to resist the specific solvents in the inks you use, so this isn’t something you can guess at—you have to match it.
Wait, one more thing: customization and future needs. A lot of small food brands start out printing 1,000 bags at a time, then scale up to 100,000. If you pick a one-size-fits-all sleeve when you’re small, you might outgrow it when you scale, and have to re-invest in new sleeves. I work with every client to map out their 1-3 year production goals. For example, a craft soda brand that started with 500 cases a month wanted to print 5,000 cases in a year. We recommended a sleeve that’s adjustable for both short runs and large runs, with a coating that can handle their water-based ink and future substrate changes (they might switch from glass bottles to aluminum cans down the line). That way, they don’t have to buy a new sleeve every time they expand, which saves them money.
Let’s wrap this up with the real stuff I wish more print guys knew: anilox sleeves aren’t just a part you swap out. For food packaging, they’re a bridge between your ink, your substrate, and your customers’ safety (and enjoyment of your product). Every choice—from food compliance to cell count to solvent matching—has a direct impact on print quality, production costs, and avoiding costly mistakes like recalls or brand damage.
Embossing Roller If you’re a food packaging printer or brand owner and you’re tired of sleeves that don’t hit the mark, or you’re worried about compliance and print consistency, let’s connect. I’ve worked with hundreds of food brands, from small craft bakeries to large snack corporations, and I can help you pick the right anilox sleeve that fits your needs, budget, and strict food safety rules. No jargon, no pushy sales tactics, just actual advice that’s tested on real packaging lines.
References
- Food and Drug Administration. (2023). Compatibility of Food Contact Substances with Printing Inks and Coatings.
- European Food Safety Authority. (2022). Scientific Opinion on Anilox Sleeve Components for Food Packaging Printing Applications.
- Flexographic Technical Association. (2021). Anilox Roll and Sleeve Specifications for Flexible Packaging Printing.
- International Organization for Standardization. (2020). ISO 15754:2020 – Packaging – Printing processes – Flexographic printing – Guidelines for anilox roll and sleeve selection.
- Gatti, L. (2022). Durability and Sanitation of Anilox Sleeves in High-Volume Food Packaging Production. Journal of Packaging Technology and Science.
Kunshan Hanhan Co., Ltd.
We’re well-known as one of the leading anilox sleeve manufacturers and suppliers in China. We warmly welcome you to buy high quality anilox sleeve made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 1093, B Zone, No. 2 Xugongqiao Rd, Huaqiao Town, Kunshan City, Suzhou, Jiangsu, China
E-mail: info@kshhroller.com
WebSite: https://www.kshh-roller.com/
